Cooler Box Bulk Purchase: A Procurement Framework
Buyers searching for cooler box bulk purchase are usually trying to solve two problems at once: what the box should cost and how to avoid paying for the wrong specification. The most useful way to compare quotations is to divide the decision into product definition, project cost, production cost, logistics, and lifecycle control. That structure makes hidden differences visible: a cheap unit may carry expensive freight, a premium unit may include engineering that another quote omits, and a strong sample may still fail commercially if the production specification is not controlled.
Prove the design before multiplying the quantity
At scale, this factor becomes less forgiving because small assumptions multiply across the order. An approved sample establishes dimensions, fit, surface, closure behavior, branding, packout compatibility, and other visible requirements that production units should reproduce. In practical terms, changes after approval can create rework, new tooling, scrapped packaging, delayed launches, or split inventory, which are often more expensive than careful sample review. The strongest final decision links the specification, evidence, commercial term, and operating consequence in one record. Freeze a signed drawing, sample reference, color standard, print artwork, carton specification, and inspection points before mass production. From an engineering standpoint, a hand-finished prototype may not represent the surface, tolerance, cycle, or material of molded production. That record also gives purchasing, quality, and operations the same reference when a later lot looks or behaves differently from the approved sample.
The strongest sourcing teams treat this as a controlled input rather than a last-minute purchasing detail. Bulk buying concentrates quality, inventory, cash, and specification risk into a larger quantity, so small ambiguities multiply quickly. Operationally, a favorable unit price can be lost through overstock, warehouse space, damage, inconsistent lots, or a late design change after thousands of units are produced. The strongest final decision links the specification, evidence, commercial term, and operating consequence in one record. Use a controlled specification, approved sample, pre-production confirmation, staged inspection, and forecast-based releases when possible. For sourcing teams, bulk purchase should scale a proven specification, not substitute volume for validation. Documenting the assumption now makes later negotiation, approval, and repeat ordering much easier.
This is where many quotations stop being comparable. For repeat orders, dimensions, lid fit, wall condition, molded defects, hardware, labels, carton strength, and cleanliness can matter as much as the initial sample. At the quotation stage, inspection and controlled production add cost, but uncontrolled variation can create packing delays, returns, damage, or a loss of confidence across a large batch. The strongest final decision links the specification, evidence, commercial term, and operating consequence in one record. Agree on measurable acceptance criteria, inspection frequency, defect handling, traceability, and what happens when a raw material, mold, component, or process changes. Commercially, generic claims such as “high quality” are not substitutes for defined acceptance criteria. That record also gives purchasing, quality, and operations the same reference when a later lot looks or behaves differently from the approved sample.
Taken together, sample-to-production control, bulk purchasing discipline, and production consistency and quality control should be treated as one sourcing conversation rather than separate afterthoughts. For cooler box bulk purchase, this matters because a supplier can only hold a price against assumptions that are visible and stable. A controlled RFQ gives the supplier room to propose alternatives while preserving the functions that the buyer has identified as non-negotiable. This does not guarantee the lowest number, but it reduces the chance of buying a cheaper specification that creates a more expensive operation.
Model volume tiers against inventory and freight
At scale, this factor becomes less forgiving because small assumptions multiply across the order. Production setup, mold heating, color preparation, printing, assembly, quality inspection, and carton packing create fixed work that is spread over the order quantity. From an engineering standpoint, larger runs can reduce the fixed cost per unit, but they also increase inventory exposure, cash tied up in stock, storage demand, and the cost of a design change. The strongest final decision links the specification, evidence, commercial term, and operating consequence in one record. Request price breaks at realistic annual volumes rather than one artificially large quantity, and ask whether repeat orders can use the same setup and packaging specification. In practical terms, the lowest tier price is not automatically the lowest total cost if demand is uncertain or product changes are likely. A useful cost-reduction discussion therefore asks which feature, setup, or volume assumption can change without damaging the operating requirement.
The strongest sourcing teams treat this as a controlled input rather than a last-minute purchasing detail. A forecast gives the supplier visibility while releases or call-offs can keep inventory closer to actual demand when both sides agree on material commitments and capacity. From an engineering standpoint, this approach can reduce repeated setup and emergency production without forcing the buyer to receive the entire annual requirement at once. The strongest final decision links the specification, evidence, commercial term, and operating consequence in one record. Discuss annual volume, release size, safety stock, raw-material commitment, cancellation rules, and the period for firm versus flexible demand. Before mass production, forecasts are useful only when the commercial agreement states which quantities are binding. A useful cost-reduction discussion therefore asks which feature, setup, or volume assumption can change without damaging the operating requirement.
The strongest sourcing teams treat this as a controlled input rather than a last-minute purchasing detail. Cooler boxes are bulky relative to their mass, so cartons, nesting ability, stacking, pallet pattern, and container utilization can strongly influence delivered cost. Operationally, a slightly cheaper unit can become more expensive after export packing and transport if it ships with excessive empty volume or needs heavy protective cartons. The strongest final decision links the specification, evidence, commercial term, and operating consequence in one record. Ask for packed carton dimensions, units per carton, gross weight, pallet pattern if used, and loading assumptions so your forwarder can compare freight on the same basis. For sourcing teams, do not infer delivered economics from factory unit price alone. For an international program, keep the factory quotation, packed shipment data, and forwarder estimate as separate inputs so a freight change does not silently rewrite the product comparison.
Taken together, order quantity and MOQ, forecast and blanket-order strategy, and freight cube and packing efficiency should be treated as one sourcing conversation rather than separate afterthoughts. For cooler box bulk purchase, this matters because a supplier can only hold a price against assumptions that are visible and stable. A controlled RFQ gives the supplier room to propose alternatives while preserving the functions that the buyer has identified as non-negotiable. Once the requirement is explicit, suppliers can propose cost reductions without quietly removing a function you actually need.
| Decision layer | Price question | Evidence to keep |
| Product | What exact cooler are we buying? | Drawing, sample and specification |
| Project | Which one-time costs apply? | Tooling, artwork and development quote |
| Production | How does price change with volume? | Tiered quote and quality plan |
| Logistics | What is the delivered cost? | Packing data, trade term and freight model |
| Lifecycle | What happens after receipt? | Reuse, storage, inspection and change controls |
The table is useful only when every supplier is answering the same requirement. Keep the underlying drawing, packing assumption, quantity, and trade-term basis with the commercial comparison so a later revision does not turn the columns into different products.
Protect the specification through production change
A supplier can quote this accurately only when the buyer defines the boundary of the requirement. A change in material grade, density, supplier, mold, wall section, component, adhesive, print process, or packing method can affect fit, durability, appearance, or thermal behavior. For sourcing teams, uncontrolled changes can trigger requalification, field complaints, repacking, or mixed inventory that costs more than a disciplined notification process. The strongest final decision links the specification, evidence, commercial term, and operating consequence in one record. Require advance notification for defined changes and agree on when a new sample, test, or approval is needed before the changed product ships. Operationally, the phrase “same product” should be defined by controlled specifications, not visual similarity alone. That record also gives purchasing, quality, and operations the same reference when a later lot looks or behaves differently from the approved sample.
The commercial effect becomes clearer when the specification is written as an operating requirement. Problems are easier to contain when incoming cartons, quantity, dimensions, lid fit, surfaces, accessories, labeling, and packaging condition are checked before the units enter normal operations. For sourcing teams, receiving inspection has a small operational cost compared with discovering a batch problem after redistribution, packing, or customer delivery. The strongest final decision links the specification, evidence, commercial term, and operating consequence in one record. Create a short incoming checklist tied to the approved sample and purchase specification, and preserve lot information for any nonconforming units. Commercially, do not rely solely on a supplier’s outgoing inspection when the cooler is critical to your process. That record also gives purchasing, quality, and operations the same reference when a later lot looks or behaves differently from the approved sample.
A supplier can quote this accurately only when the buyer defines the boundary of the requirement. Custom molded shapes, handles, hinge features, logos, lid geometry, inserts, and integrated details can require dedicated tooling or mold modification. In practical terms, tooling may be quoted separately, amortized into unit price, or shared across a forecast, so two low-looking quotations can have very different economics over the planned volume. The strongest final decision links the specification, evidence, commercial term, and operating consequence in one record. Ask who owns the tooling, what changes are included, what triggers a new tool, how maintenance is handled, and whether the tool can support future volume or design revisions. At the quotation stage, a cheap first sample does not prove that the production tool, cycle, material, and tolerances will be the same. A useful cost-reduction discussion therefore asks which feature, setup, or volume assumption can change without damaging the operating requirement.
Taken together, change control, receiving inspection, and tooling and mold economics should be treated as one sourcing conversation rather than separate afterthoughts. For cooler box bulk purchase, this matters because a supplier can only hold a price against assumptions that are visible and stable. A controlled RFQ gives the supplier room to propose alternatives while preserving the functions that the buyer has identified as non-negotiable. This does not guarantee the lowest number, but it reduces the chance of buying a cheaper specification that creates a more expensive operation.
Match insulation and coolant to the actual route
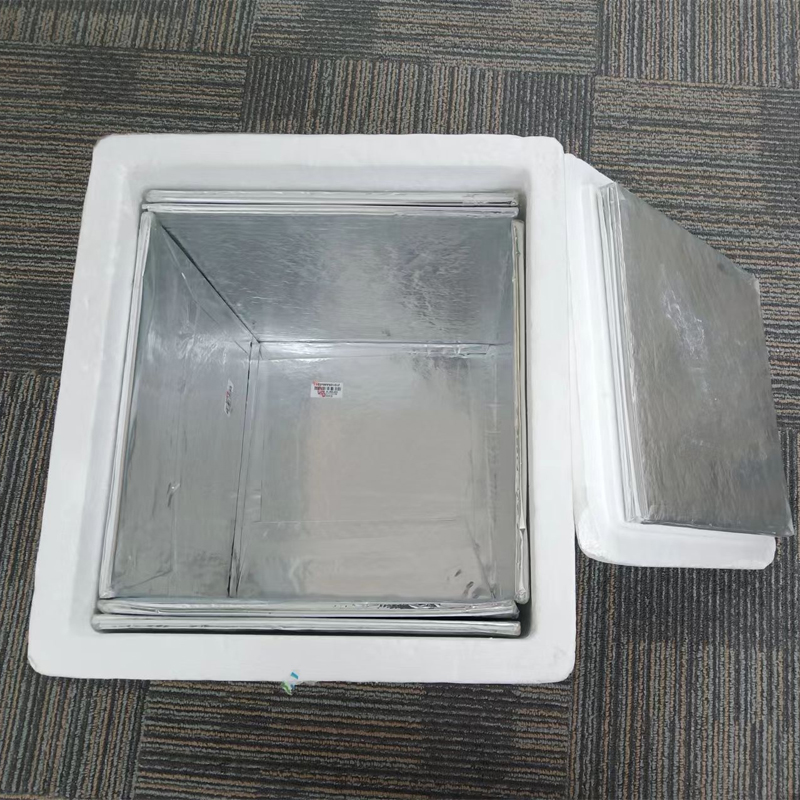
The strongest sourcing teams treat this as a controlled input rather than a last-minute purchasing detail. The thermal path depends on wall material, wall thickness, joints, lid fit, closures, internal air space, and how coolant surrounds the payload. Before mass production, thicker or more complex insulation consumes more material and may increase outside dimensions, which can raise packing and freight cost even when the internal payload volume stays the same. The strongest final decision links the specification, evidence, commercial term, and operating consequence in one record. Ask for internal and external dimensions together, plus drawings or samples that show the lid joint, wall section, and usable payload space. Operationally, a material with better laboratory insulation properties can still perform poorly if the complete box has leakage paths, large empty spaces, or an unsuitable packout. For that reason, drawings and physical samples usually tell procurement more than a product name or nominal capacity alone.
Helpful decision tools
Check the details before you choose packaging
These quick tools can help you compare route risk, sizing needs, coolant choices, and packaging details before you request a quote.
Route Risk Checker
Review lane conditions before selecting packaging for real operating requirements.
Check route riskDry Ice Calculator
Estimate dry ice needs for frozen or ultra-cold shipments before packing.
Estimate dry iceInsulation Material Reference
Compare insulation material choices for different cold chain packaging needs.
Compare materialsThis is where many quotations stop being comparable. Gel packs, ice bricks, phase change materials, water ice, or dry ice are separate cooling components whose conditioning and placement affect the complete thermal system. For a repeat-order program, a quote for the cooler alone may look low until coolant quantity, conditioning labor, separators, absorbent materials, liners, and replacement stock are added. The strongest final decision links the specification, evidence, commercial term, and operating consequence in one record. Clarify whether coolant is included, optional, or supplied by you, and request a repeatable packout instruction if temperature control is part of the project. From an engineering standpoint, the box is the insulating enclosure; the coolant supplies cooling capacity. Neither should be evaluated in isolation for a temperature-sensitive route. If the shipment is temperature-sensitive, the approval record should state the payload, coolant condition, packing sequence, monitoring method, and the route or test profile used to judge acceptance.
This factor is easy to overlook because it often sits outside the headline unit price. For temperature-sensitive shipping, performance depends on the complete configuration: enclosure, coolant, payload, conditioning, pack pattern, ambient exposure, route, and operating procedure. For sourcing teams, development testing, laboratory work, documentation, and repeat studies after major design changes can be real project costs even when they are not part of the molded box price. The strongest final decision links the specification, evidence, commercial term, and operating consequence in one record. Ask what test method, ambient profile, payload, coolant, acceptance criteria, and sample configuration support any performance statement. For formal cold-chain programs, determine whether standards such as ISTA thermal methods are relevant to your quality process. Commercially, a stated hold time should never be treated as universal unless the test conditions match the intended use. If the shipment is temperature-sensitive, the approval record should state the payload, coolant condition, packing sequence, monitoring method, and the route or test profile used to judge acceptance.
Taken together, insulation architecture, coolant and packout, and thermal and transport evidence should be treated as one sourcing conversation rather than separate afterthoughts. For cooler box bulk purchase, this matters because a supplier can only hold a price against assumptions that are visible and stable. A controlled RFQ gives the supplier room to propose alternatives while preserving the functions that the buyer has identified as non-negotiable. That approach makes the final price easier to explain internally and easier to defend during supplier review.
Use a bulk sourcing scorecard that includes total cost
This is where many quotations stop being comparable. A meaningful comparison uses the same internal dimensions, material family, wall or shell structure, accessories, customization, packing method, quantity, trade term, and quality requirements. Before mass production, when these inputs differ, the price gap may reflect a different product rather than a more or less competitive supplier. The strongest final decision links the specification, evidence, commercial term, and operating consequence in one record. Create a comparison sheet that records included and excluded items, one-time charges, sample cost, tooling, carton packing, spare parts, and freight basis. Commercially, a unit price without a controlled specification is only a preliminary number. Documenting the assumption now makes later negotiation, approval, and repeat ordering much easier.
The strongest sourcing teams treat this as a controlled input rather than a last-minute purchasing detail. Landed cost links factory price with export packing, origin charges, international freight, insurance if applicable, customs-related charges, duties or taxes, destination handling, local delivery, and inventory effects. For sourcing teams, bulky insulated products can shift the economics toward shipping efficiency, especially when freight is priced by volume rather than actual mass. The strongest final decision links the specification, evidence, commercial term, and operating consequence in one record. Build a per-unit landed-cost worksheet using the supplier packing data and your own forwarder or customs information rather than asking the manufacturer for a single universal landed number. Operationally, duty rates and taxes depend on classification, origin, destination, and current rules, so they should be verified for the specific transaction. For an international program, keep the factory quotation, packed shipment data, and forwarder estimate as separate inputs so a freight change does not silently rewrite the product comparison.
The strongest sourcing teams treat this as a controlled input rather than a last-minute purchasing detail. Deposits, balance timing, tooling payments, sample charges, inspection holds, and payment method determine how much cash is committed before goods are received. From an engineering standpoint, a small unit-price discount can be offset by unfavorable cash timing, financing cost, or the risk of paying too much before acceptance evidence is available. The strongest final decision links the specification, evidence, commercial term, and operating consequence in one record. Compare payment terms alongside price and define what documentation or inspection releases each payment milestone. For a repeat-order program, commercial terms should be reviewed with the buyer’s finance and legal teams, especially for new suppliers or large custom programs. Documenting the assumption now makes later negotiation, approval, and repeat ordering much easier.
The strongest sourcing teams treat this as a controlled input rather than a last-minute purchasing detail. Lead time can include tooling, sampling, artwork, material preparation, molding, secondary operations, inspection, carton production, export booking, and seasonal factory loading. Operationally, rush production or split shipments can erase a unit-price advantage, while large safety stocks can increase carrying cost and hide quality problems until too much inventory is built. The strongest final decision links the specification, evidence, commercial term, and operating consequence in one record. Ask for a milestone schedule, identify long-lead items, and separate sample, tooling, mass-production, and shipping lead times instead of relying on one headline number. From an engineering standpoint, a quoted lead time is only useful when its start point, assumptions, and approval gates are clear. Documenting the assumption now makes later negotiation, approval, and repeat ordering much easier.
Taken together, quotation normalization, landed cost modeling, payment terms and cash exposure, and lead time and production planning should be treated as one sourcing conversation rather than separate afterthoughts. For cooler box bulk purchase, this matters because a supplier can only hold a price against assumptions that are visible and stable. A controlled RFQ gives the supplier room to propose alternatives while preserving the functions that the buyer has identified as non-negotiable. That approach makes the final price easier to explain internally and easier to defend during supplier review.
Practical example
Imagine a distributor expects a large seasonal program and receives a strong price at a very high quantity. The tempting response is to buy the entire forecast at once. A more controlled approach is to confirm the production sample, carton loading, storage requirement, receiving plan, and sell-through assumptions first. If the supplier can reserve capacity or materials under a blanket arrangement, the buyer may capture part of the scale benefit without accepting all finished-goods inventory on day one. The right structure depends on the commercial agreement, but the example shows why bulk price should be linked to inventory behavior rather than treated as an isolated discount.
Frequently asked questions
How large should the first bulk cooler box order be?
There is no universal quantity. The first production order should reflect demand, storage, cash flow, design confidence, and supplier capability. A common discipline is to approve a representative sample, verify packing and critical dimensions, confirm production controls, and then scale volume in a way that does not create unnecessary inventory or lock the buyer into an unproven design.
What should be inspected in a large cooler box batch?
Inspection points should follow the approved specification. Typical checks may include dimensions, lid fit, surface condition, molded defects, hardware, branding, accessory count, carton condition, labeling, and cleanliness. Temperature-sensitive programs may also require separate packout or thermal verification. The exact plan should reflect the consequences of a defect in your operation.
Are reusable cooler boxes always cheaper for bulk programs?
Not always. Reuse can improve economics when return logistics, cleaning, inspection, storage, and loss control are manageable. If units do not come back reliably, if cleaning is difficult, or if reverse transport is expensive, the expected number of successful cycles may be too low. Compare cost per successful use rather than purchase price alone.
How can buyers reduce risk when committing to a large quantity?
Use a controlled drawing and sample, agree on measurable acceptance criteria, document packaging, require change notification, and consider staged inspections or releases. Forecast or blanket-order structures can sometimes provide scale benefits while avoiding the need to receive the entire annual quantity at once, but the commercial terms should clearly state what is binding.
Conclusion
A credible answer to cooler box bulk purchase is built from a controlled specification rather than a universal price range. Define usable space and construction first, separate tooling and customization from recurring unit cost, normalize quantity and packing assumptions, and calculate delivered economics on the same trade-term basis. If the cooler is part of a temperature-sensitive shipment, require evidence for the complete packout instead of treating the insulation material as proof. Finally, protect the approved design through production quality and change control. Those steps give purchasing a price that can be compared, explained, and repeated.
About Tempk
Tempk supplies cold-chain packaging products including EPP cooler boxes and insulated shipping solutions for food, grocery, pharmacy, and logistics applications. Public product information shows project options such as custom size, wall thickness, color, logo, inserts, dividers, labels, coolant matching, and packing method. For buyers discussing price, the useful starting point is a project brief that defines payload, route, coolant, customization, order quantity, and packing expectations. Temperature performance or qualification should then be reviewed against the specific packout and supporting evidence rather than assumed from the box material alone.
Next step: For a cleaner supplier comparison, send Tempk one controlled RFQ covering the product, quantity tiers, packing, delivery term, and evidence required before production approval.